Best Vibratory Feeders & Flow-Aid Equipment Manufacturer in Indore
- posted by: Indpro Engineers
- No Comments
Material flow problems are a persistent worry in all industries that deal with bulk solids, such as chemicals, food, cement, and pharmaceuticals. Sticking, bridging, and clogging are common issues that cause severe operational difficulties in powders and granular materials stored in bins, hoppers, or silos, including:
- Unpredictable material release
- Production downtime
- Labor-intensive manual intervention
- Equipment damage due to inconsistent feeding
At this point, it is necessary to introduce specialized machinery such as Vibrating Bin Aerator, Vibratory Spiral Elevator, and Vibrating Bin Discharger to facilitate efficient handling of the material.
The Issue: Material Flow Not Dependable
Poor flow properties powders include flour, cement, chemicals, and minerals. Moisture, the shape of particles, and the geometry of bins cause them to compact and adhere to the walls of bins. The conventional discharge systems lack the ability to maintain a constant flow, and it leads to
- Obstructed discharge outlets
- Production interruptions
- Higher downtime expenses
- Workplace safety risks to employees
The Solution: Advanced Flow-Aid Equipment
1️⃣ Vibrating Bin Aerator: Shattering Bridges and Recovering Flow
Vibrating Bin Aerator is a very basic and, at the same time, very efficient device that is fitted into storage bins. It applies an air and vibration combination to:
- Avoid material compaction.
- Destroyed bridges or rat holes formed
- Maintain the uninterrupted supply of powder or granular substance.
The vibrating bin aerator helps in keeping the material loose and fluidized, thus eliminating the scenarios of poking or hammering of bins manually; this is not only dangerous but also inefficient.
2️⃣ Vibratory Spiral Elevator: Vertical Conveying Made Practical
The Vibratory Spiral Elevator is an ideal choice when the materials are to be elevated to upper processing levels. and whereas belt conveyors or screw lifts are more space-consuming and more subject to maintenance, the vibratory spiral elevator:
- Compact footprint vertical material movement
- Transportation of delicate products without humiliation
- Minimizes dust creation because of regulated vibration
- Has few moving parts, and therefore minimal maintenance is required.
3️⃣ Vibrating Bin Discharger: Repeatable Discharge
A Vibrating Bin Discharger is placed on the outlet of the bins or silos. Its Tempered vibration.
- Loose compacted materials
- Assured consistent and uniform discharge
- Eliminates wild surges or stoppages of flow
- Lengthens machine life through the lessening of mechanical tension
The Outcome: Smooth, Dependable Material Movement
With the Vibrating Bin Aerator, Vibratory Spiral Elevator, and Vibrating Bin Discharger incorporated into your plant, you can forget about problems with material flows, ensure less downtime, higher safety, and overall optimization of the entire production process.
Contact Us for More Info
FAQ About Vibratory Feeders
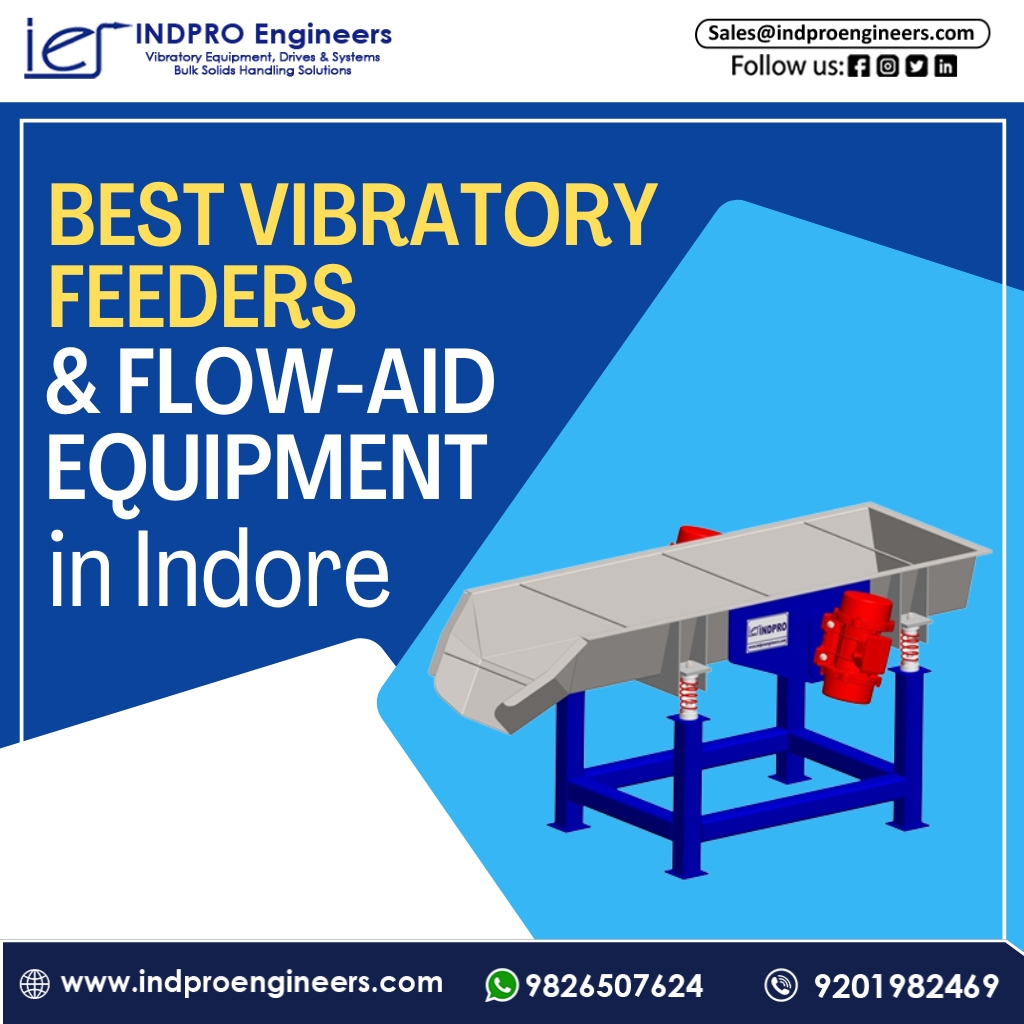
A vibratory feeder is used to move and control the flow of bulk materials from storage or feeding equipment to the next stage of a production process. It provides a consistent and controlled material flow.
Flow-aid equipment helps improve the movement of bulk materials through bins, hoppers, and silos. It can reduce issues such as bridging, clogging, and material buildup, supporting smooth and reliable material handling.
Vibratory feeders are widely used in food processing, chemicals, pharmaceuticals, mining, cement, plastics, glass, packaging, and other industries that handle bulk materials.
INDPRO Engineers provides vibratory feeders and flow-aid equipment designed for efficient and reliable bulk material handling. Its solutions can be selected according to material characteristics, capacity, and specific process requirements.